Oct . 26, 2025 10:40 Back to list
Runout Tester – Ultra-Precise, Fast-Setup Industrial Gauge
A Field Insider’s Take on the Runout Tester
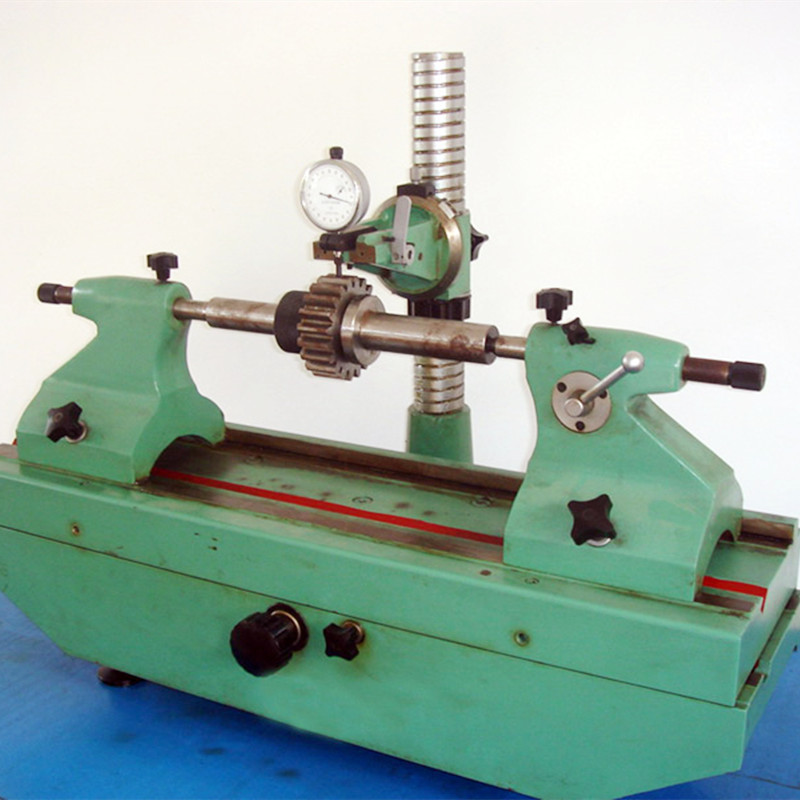
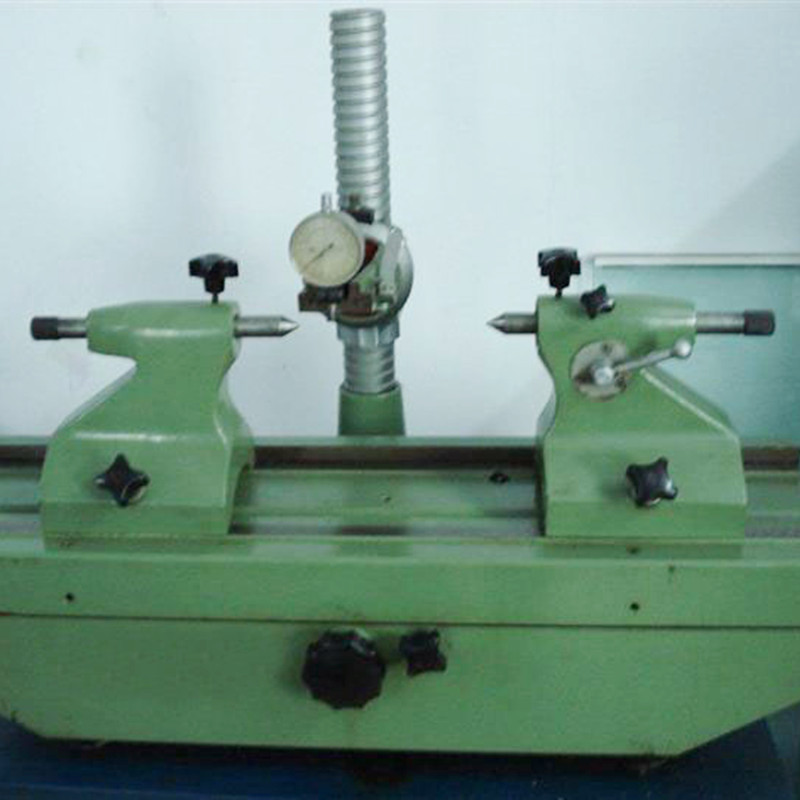
If you machine shafts for a living—camshafts, pump rotors, e-motor spindles—you already know: runout is the quiet saboteur. The good news is that a well-built Runout Tester turns geometry from guesswork into clarity. This pendulum-style bench instrument locates parts between two hardened centers (thimbles), you rotate the work, and the probe shows true radial error. Simple idea, surprisingly revealing.
What’s trending in runout control
Two shifts are obvious: tighter GD&T across EV and precision hydraulics, and traceable data. Plants want microns—and proof. That’s pushing testers toward higher-resolution probes, quick-change centers, and optional digital logging. Honestly, the analog dial isn’t going away (operators trust it), but pairing it with an LVDT and a USB logger is becoming normal.
Core specs (field-proven, operator-friendly)
| Measurement range | ≈0–1 mm (analog dial), up to 0–5 mm with LVDT; real-world use may vary |
| Resolution | 1 µm (0.001 mm) typical; 0.5 µm optional |
| Between-centers distance | ≈50–500 mm adjustable (extensions available) |
| Centers (thimbles) | 60° hardened steel, HRC 58–62; quick-swap tips |
| Base | Cast iron or granite, straightness ≈3 µm/300 mm |
| Repeatability | ≤1–2 µm under stable conditions |
| Certifications | ISO 9001 facility; CE; calibration traceable to ISO/IEC 17025 |
| Service life | ≈5–10 years with periodic calibration |
How it’s used (quick process flow)
- Materials: typical shafts in 42CrMo, 4140, stainless, or tool steel; journals lightly oiled.
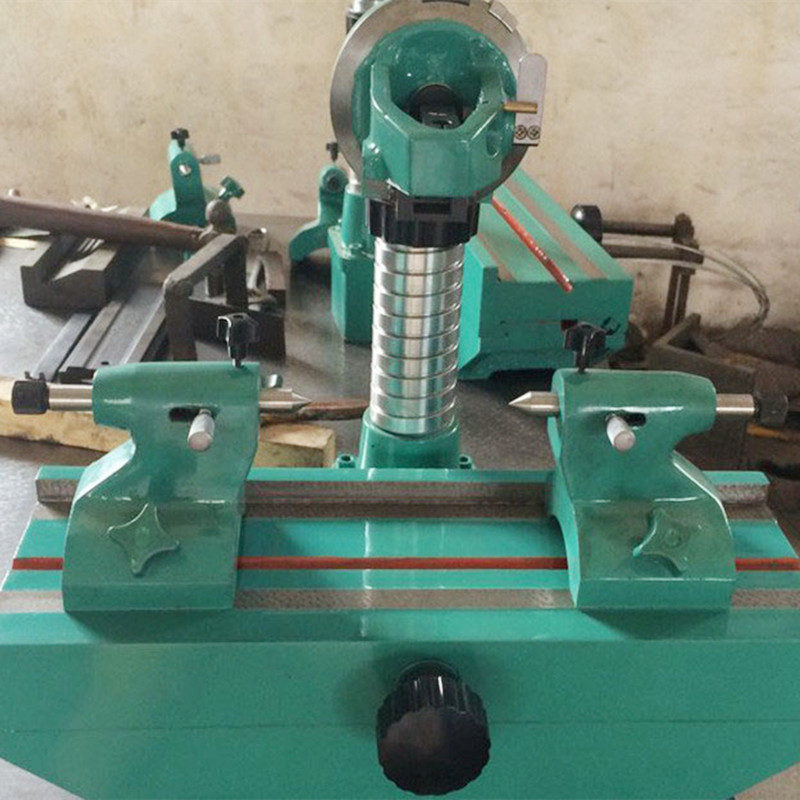
- Setup: mount part between centers; set probe at the critical journal; zero indicator.
- Method: rotate by hand (or low-speed motor). Note TIR at each station.
- Standards: interpret per ISO 1101 (circular/total runout); verify method with ISO 230-1; many shops reference ASME Y14.5/ASME B89 for metrology practice.
- Decision: compare TIR to drawing tolerance; log pass/fail and value.
- Service: wipe ways, check center wear weekly; annual calibration recommended.
Where it fits
Automotive powertrain, aerospace build shops, pump/valve makers, e-mobility motors, machine tool spindles, even medical mandrels. Many customers say the Runout Tester pays for itself by catching bent stock early—before it hits a grinder.
Why this model stands out
- Direct radial readout; low learning curve.
- Rigid base; stable zero (less needle “drift”).
- Analog or LVDT probe; optional data capture.
- Centers/fixtures configurable for odd geometries.
Vendor snapshot (quick comparison)
| Vendor | Accuracy/Repeatability | Lead time | Customization | Approx. price |
|---|---|---|---|---|
| STR Machinery (Cangzhou, China) | ≈1–2 µm repeatability | 2–4 weeks | High (centers, probes, base) | Budget-friendly |
| Vendor A (Japan) | ≈1 µm repeatability | 6–10 weeks | Medium | Premium |
| Vendor B (EU) | ≈1–2 µm repeatability | 4–8 weeks | Medium–High | Upper mid-range |
Customization options
Swap in carbide centers for abrasive parts, add a granite base for thermal stability, or pick a 0.5 µm LVDT with a simple logger. STR can also adapt fixtures for stepped shafts or keyways—handy, actually, when parts aren’t textbook-perfect.
Real-world notes (mini case studies)
- Automotive camshaft cell: average TIR tightened from 0.018 mm to 0.010 mm; scrap reduced ≈18% over 3 months (n=420 parts).
- Hydraulic pump rotors: early bend detection saved a grinder wheel per month; operators liked the analog dial better for quick triage.
- E-motor shafts: with LVDT logging, PPAP evidence became painless—quality manager’s words, not mine.
Origin: No.17, Building 11, Hardware Building Material City, Botou, Cangzhou City, Hebei Province, China. Many buyers mention responsive after-sales and straightforward calibration support.
Standards and compliance
Use per ISO 1101 for circular/total runout interpretation; verify method against ISO 230-1; align drawings with ASME Y14.5. For audits, keep calibration certificates traceable to ISO/IEC 17025. It sounds formal, but it saves headaches.
- ISO 1101: Geometrical tolerancing—Geometrical tolerances of form, orientation, location and run-out. ISO, latest edition.
- ISO 230-1: Test code for machine tools—Part 1: Geometric accuracy of machines operating under no-load or quasi-static conditions. ISO.
- ASME Y14.5: Dimensioning and Tolerancing; and ASME B89 series for measurement practice. ASME.
-
Ball Check Valve Questions About Connection, Parts and MaintenanceNewsNov.02,2026
-
Butterfly Valve Wholesale FAQ: Types, Specifications & Selection QuestionsNewsOct.28,2026
-
Choosing Guide Rail: Application Fit and Specification ChecksNewsOct.23,2026
-
Choosing a Measuring Micrometer: Application Fit and Specification ChecksNewsOct.23,2026
-
Choosing a Level Ruler: Application Fit and Specification ChecksNewsOct.23,2026
-
Choosing a Ring Gauge: Application Fit and Specification ChecksNewsOct.23,2026
 Afrikaans
 Albanian
 Amharic
 Arabic
 Armenian
 Azerbaijani
 Basque
 Belarusian
 Bengali
 Bosnian
 Bulgarian
 Catalan
 Cebuano
 Corsican
 Croatian
 Czech
 Danish
 Dutch
 Esperanto
 Estonian
 Finnish
 French
 Frisian
 Galician
 Georgian
 German
 Greek
 Gujarati
 Haitian Creole
 Hausa
 Hawaiian
 Hebrew
 Hindi
 Miao
 Hungarian
 Icelandic
 Igbo
 Indonesian
 Irish
 Italian
 Japanese
 Javanese
 Kannada
 Kazakh
 Khmer
 Rwandese
 Korean
 Kurdish
 Kyrgyz
 Lao
 Latin
 Latvian
 Lithuanian
 Luxembourgish
 Macedonian
 Malgashi
 Malay
 Malayalam
 Maltese
 Maori
 Marathi
 Mongolian
 Myanmar
 Nepali
 Norwegian
 Norwegian
 Occitan
 Pashto
 Persian
 Polish
 Portuguese
 Punjabi
 Romanian
 Russian
 Samoan
 Scottish Gaelic
 Serbian
 Sesotho
 Shona
 Sindhi
 Sinhala
 Slovak
 Slovenian
 Somali
 Spanish
 Sundanese
 Swahili
 Swedish
 Tagalog
 Tajik
 Tamil
 Tatar
 Telugu
 Thai
 Turkish
 Turkmen
 Ukrainian
 Urdu
 Uighur
 Uzbek
 Vietnamese
 Welsh
 Bantu
 Yiddish
 Yoruba
 Zulu
 English