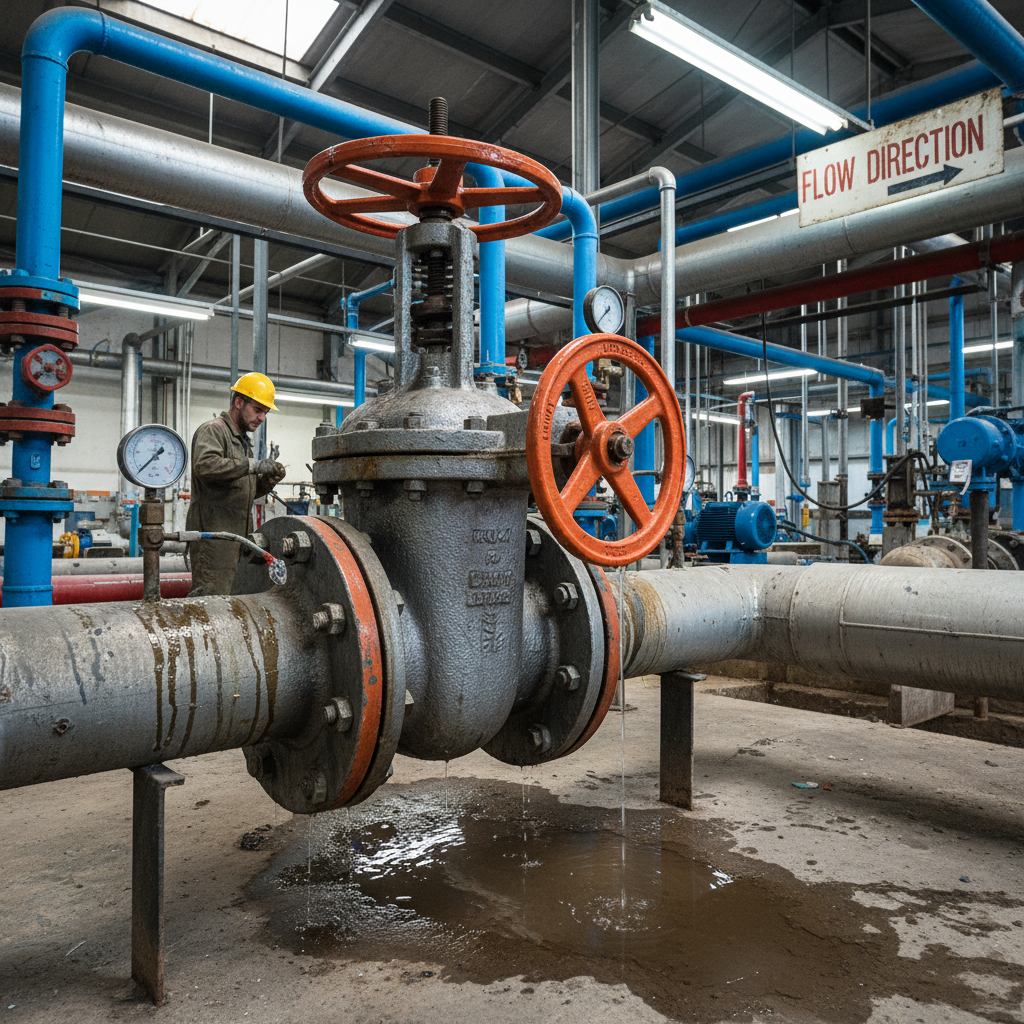
Selecting a reliable valve manufacturer is a critical decision for any industrial operation that relies on fluid control, pressure management, and system safety. In the complex landscape of general equipment manufacturing, valves serve as the primary guardians of operational integrity, ensuring that liquids and gases are transported efficiently while preventing catastrophic leaks or system failures.
The global demand for precision-engineered valves has surged as industries like oil and gas, chemical processing, and water treatment evolve toward higher pressure tolerances and more corrosive environments. A professional valve manufacturer does not simply cast metal; they integrate advanced metallurgy, tight tolerance machining, and rigorous testing protocols to meet international ISO and API standards.
Understanding the nuances of valve production—from material selection to the final pressure test—allows procurement managers and engineers to optimize their supply chains for longevity and safety. By partnering with a specialized manufacturer, companies can reduce downtime and ensure that their infrastructure remains compliant with evolving environmental and safety regulations across the globe.
The Strategic Role of a Valve Manufacturer in Modern Industry
A leading valve manufacturer acts as the backbone of industrial safety. By specializing in the creation of components that regulate flow, these manufacturers ensure that critical systems—ranging from municipal water grids to high-pressure steam lines in power plants—operate within safe parameters. The strategic importance lies in the precision of the seal; a fraction of a millimeter in variance can lead to significant energy loss or hazardous leaks.
Furthermore, the ability of a manufacturer to customize alloy compositions allows industries to combat specific environmental threats, such as saltwater corrosion in offshore drilling or chemical erosion in pharmaceutical labs. This technical agility transforms a simple supplier into a strategic partner, providing the necessary hardware to push the boundaries of industrial efficiency and safety.
Defining the Scope of Valve Manufacturing and Engineering
In simple terms, a valve manufacturer is an entity that designs, casts, machines, and tests mechanical devices used to start, stop, or modulate the flow of a fluid. This includes a vast array of designs such as ball, gate, globe, butterfly, and check valves. The process is a blend of heavy industrial casting and micron-level precision machining, requiring a deep understanding of fluid dynamics and material science.
Modern valve manufacturing is inextricably linked to humanitarian and societal needs. For instance, the reliable delivery of clean drinking water to urban populations depends entirely on the durability of valves installed in underground piping. When these components fail, the result is not just financial loss but a potential public health crisis, highlighting the ethical responsibility of the manufacturer to produce zero-defect hardware.
Beyond basic flow control, the scope has expanded to include "intelligent" valves. These are integrated with sensors and actuators that allow for remote monitoring and automated adjustments. This evolution means that the contemporary manufacturer must be as proficient in software integration and electronic signaling as they are in traditional metallurgy and CNC machining.
Core Components and Technical Pillars of Quality Valves
Durability is the foremost pillar for any reputable valve manufacturer. This is achieved through the rigorous selection of materials, such as stainless steel, duplex alloys, or specialized polymers, which must withstand the specific temperature and pressure gradients of the intended application. A durable valve reduces the total cost of ownership by extending the mean time between failures (MTBF).
Precision Sealing is where the expertise of a valve manufacturer truly manifests. Whether utilizing soft seats for tight shut-off or metal-to-metal seats for high-temperature stability, the seal must prevent "leakage class" failures. This requires advanced grinding and lapping processes to ensure that mating surfaces are perfectly flush, eliminating any path for fluid escape.
Scalability and Standardization ensure that components can be easily replaced or upgraded. By adhering to global standards like ASME or DIN, a manufacturer ensures that their valves are compatible with existing piping infrastructure worldwide. This interoperability is essential for global logistics, allowing a plant in Southeast Asia to source high-quality components from a manufacturer in Europe or North America without fearing fitment issues.
Global Applications and Industrial Use Cases
The practical application of products from a valve manufacturer spans nearly every sector of the global economy. In the energy sector, high-pressure valves are used in fracking and refining processes to manage volatile hydrocarbons. In the food and beverage industry, "hygienic" valves are employed to ensure that no bacteria can grow in "dead legs" of the piping, maintaining strict FDA compliance.
In remote industrial zones, such as Arctic mining operations or deep-sea oil rigs, the demand for "extreme-service" valves is paramount. These components must operate flawlessly in temperatures as low as -50°C or as high as 800°C. Similarly, in post-disaster relief operations, rapid-deployment water filtration systems rely on lightweight yet robust valve assemblies to deliver potable water to affected populations quickly.
Performance Comparison of Valve Manufacturer Standards
Tangible Advantages of High-Precision Valve Sourcing
The most immediate benefit of partnering with a premium valve manufacturer is the drastic reduction in operational risk. When a valve is engineered for the exact pressure and temperature of a system, the likelihood of "blow-out" or fatigue-induced failure is minimized. This translates to a safer working environment for employees and a lower risk of environmental contamination.
Beyond safety, there is a significant economic argument for quality. While low-cost alternatives may seem attractive, the long-term value of precision valves is found in their energy efficiency. A valve that provides a perfect seal prevents "internal leakage," meaning pumps don't have to work harder to compensate for lost pressure, leading to lower electricity costs and a reduced carbon footprint over the equipment's lifecycle.
Future Trends in Digital and Sustainable Valve Tech
The industry is currently undergoing a digital transformation known as "Valve 4.0." A forward-thinking valve manufacturer is now integrating IoT (Internet of Things) sensors directly into the valve body. These sensors can detect acoustic signatures of leaks or changes in friction that signal an impending failure, moving the industry from reactive maintenance to predictive maintenance.
Sustainability is also driving material innovation. We are seeing a shift toward additive manufacturing (3D printing) for complex internal geometries that were previously impossible to cast. This allows for "flow-optimized" valves that reduce turbulence and pressure drop, significantly increasing the overall efficiency of the fluid system and reducing energy waste.
Additionally, the rise of green hydrogen as a fuel source is challenging manufacturers to develop valves that can handle hydrogen embrittlement. This requires new alloy formulations and specialized coatings to prevent the gas from penetrating the metal lattice, ensuring that the transition to clean energy is supported by safe and reliable hardware.
Overcoming Challenges in Valve Procurement and Maintenance
One of the primary challenges in the industry is the "specification gap," where the valve ordered does not perfectly match the actual field conditions. This often happens due to poor communication between the engineering team and the valve manufacturer. The solution lies in the adoption of BIM (Building Information Modeling) and digital twins, allowing for virtual testing before a single piece of metal is cast.
Another hurdle is the degradation of valves in highly corrosive environments, which often leads to premature replacement. Expert manufacturers are addressing this by offering advanced surface treatments, such as Tungsten Carbide coating or PVD (Physical Vapor Deposition), which provide an impenetrable barrier against aggressive chemicals, extending the valve's life by several years.
Finally, supply chain volatility can lead to long lead times for custom valves. To mitigate this, many manufacturers are implementing modular design philosophies. By standardizing the valve body and customizing only the internal "trim," they can significantly reduce delivery times without compromising the specific performance requirements of the client.
Comparative Analysis of Valve Manufacturing Solutions
| Solution Type |
Material Focus |
Primary Benefit |
Reliability Score (1-10) |
| Standard Industrial |
Cast Iron / Carbon Steel |
Cost Efficiency |
7 |
| Corrosion Resistant |
316L Stainless / Hastelloy |
Chemical Stability |
9 |
| High-Pressure Extreme |
Forged Alloy Steel |
Burst Prevention |
10 |
| Hygienic / Sanitary |
Polished Stainless Steel |
Contamination Control |
8 |
| Smart Automated |
Composite / Alloy |
Predictive Maintenance |
9 |
| Cryogenic Service |
Austenitic Stainless |
Low-Temp Ductility |
9 |
FAQS
Look for a manufacturer that provides full material traceability (Mill Test Reports) and adheres to ASME B16.34 standards. A qualified manufacturer should offer hydrostatic and pneumatic testing certifications for every unit to ensure the valve can handle the maximum allowable working pressure (MAWP) without deformation or leakage.
Cast valves are made by pouring molten metal into a mold, making them cost-effective for large diameters and complex shapes. Forged valves are hammered into shape, resulting in a denser grain structure with fewer internal voids. Forged valves are generally stronger and preferred by manufacturers for high-pressure or critical safety applications.
Yes, professional manufacturers specialize in custom metallurgy. If your process involves highly corrosive acids or extreme temperatures, they can suggest alloys like Monel, Inconel, or Duplex stainless steel and provide custom coatings to ensure the hardware does not degrade prematurely in your specific environment.
Service intervals depend on the cycle count and the medium being transported. However, a general rule is an annual inspection for critical valves. Many modern manufacturers now offer "smart" valves with sensors that notify you exactly when a seal is wearing down, eliminating the need for arbitrary calendar-based maintenance.
Yes. Sustainable manufacturing focuses on reducing "leakage emissions" (fugitive emissions). A high-end valve manufacturer produces "Low-E" valves that meet stringent environmental standards, preventing harmful gases from escaping into the atmosphere, which is critical for companies striving for Net Zero goals.
At a minimum, verify ISO 9001 for quality management. Depending on the industry, look for API 6D (for pipeline valves), CE marking for European markets, and SIL (Safety Integrity Level) certifications if the valves are part of an automated safety instrumented system (SIS).
Conclusion
Selecting a competent valve manufacturer is far more than a simple procurement task; it is an investment in the safety and efficiency of your entire industrial infrastructure. From the meticulous selection of alloys to the implementation of IoT-driven predictive maintenance, the quality of your flow control components directly dictates your operational uptime and environmental compliance. By focusing on precision engineering, global standardization, and material durability, businesses can mitigate risks and optimize their long-term ROI.
As we move toward a future of green hydrogen and fully automated factories, the role of the manufacturer will evolve from a hardware provider to a full-service engineering partner. We recommend that industrial operators prioritize partners who invest in R&D and sustainable manufacturing practices to ensure their systems are future-proof. For those seeking industry-leading precision and reliability in flow control, we invite you to explore our specialized solutions. Visit our website: www.strmachinery.com